Chuyên sâu trong lĩnh vực vật liệu rời công nghiệp, cung cấp giải pháp môi trường thông minh tích hợp cho phối trộn tự động, cấp liệu tập trung, khử lưu huỳnh và khử nitơ khô!
When it comes to transporting sodium carbonate, various methods are employed across different industries. Understanding the common approaches and the specific advantages of advanced systems like those offered by Shandong HeadPowder Engineering Co., Ltd. is crucial for optimizing material handling processes. This article explores the prevalent sodium carbonate conveying methods and highlights the key benefits of HeadPowder's pneumatic conveying solutions.

Overview of Common Sodium Carbonate Conveying Methods
Sodium carbonate, also known as soda ash, is widely used in industries such as glass manufacturing, chemical production, and water treatment. The choice of conveying method depends on factors like material properties, distance, and operational requirements. Traditional methods include mechanical conveyors like belt conveyors, screw conveyors, and bucket elevators. These systems are effective for bulk material transport but may face challenges with dust control, maintenance, and suitability for fine powders. For example, belt conveyors are suitable for larger particles but can struggle with sodium carbonate's fine, dusty nature, leading to material loss and operational inefficiencies.
HeadPowder's Pneumatic Conveying System: A Modern Solution
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in developing and implementing advanced pneumatic conveying systems tailored for sodium carbonate. The company's approach focuses on efficiency, reliability, and minimal environmental impact. Pneumatic conveying uses compressed air to transport materials through a pipeline, offering several advantages over traditional mechanical methods. One of the primary benefits is the ability to handle fine powders without the need for additional dust suppression equipment. This reduces material loss and improves overall process safety.
Key Advantages of HeadPowder's Pneumatic Conveying
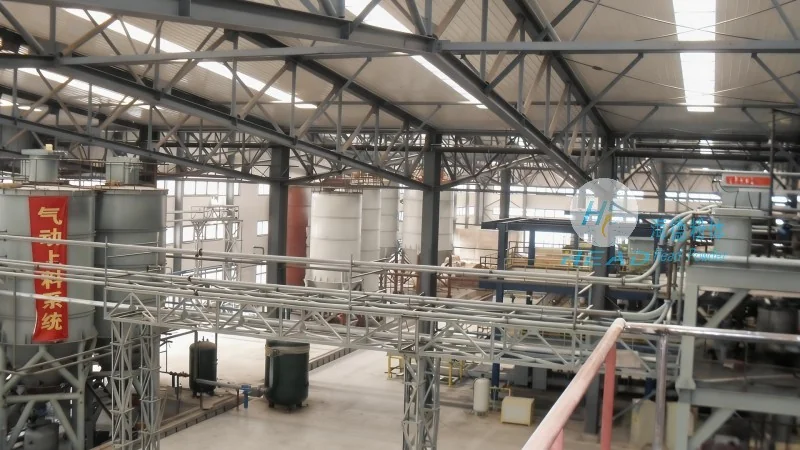
HeadPowder's pneumatic conveying systems are designed to address the unique challenges of sodium carbonate transport. The system incorporates features like positive pressure or negative pressure operation, depending on the specific application requirements. This flexibility allows for customized solutions that meet the needs of different industrial settings. Another significant advantage is the reduced risk of contamination and cross-contamination compared to mechanical systems. Pneumatic conveyors can be integrated with closed-loop systems, ensuring that the material remains contained throughout the transport process. This is particularly important for sodium carbonate, which is often used in food and pharmaceutical applications where purity is critical.
Efficiency and Cost-Effectiveness

From an operational perspective, HeadPowder's pneumatic conveying systems offer substantial efficiency gains. The use of compressed air allows for continuous, uninterrupted material flow, minimizing downtime and increasing productivity. Unlike mechanical conveyors that may require frequent maintenance and cleaning, pneumatic systems are generally more reliable and require less maintenance. This translates into lower operational costs over the long term. Additionally, the ability to transport sodium carbonate over longer distances without the need for intermediate transfer points reduces the complexity of the overall material handling system.
Environmental Considerations
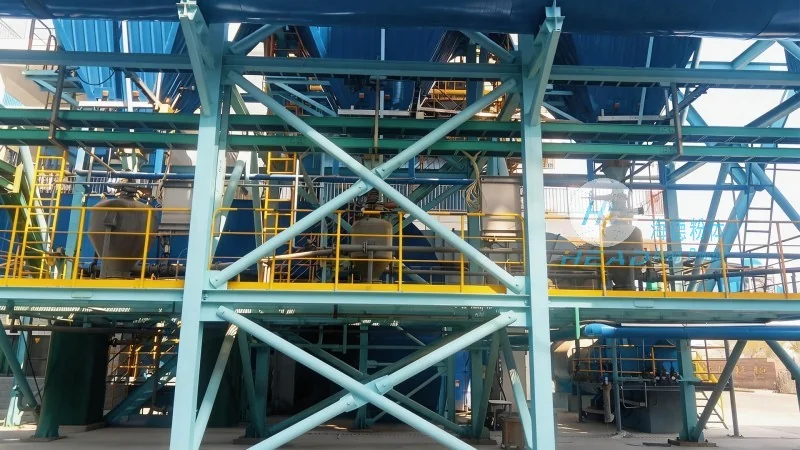
In today's industrial landscape, environmental sustainability is a key consideration for many companies. HeadPowder's pneumatic conveying systems contribute to a greener operation by minimizing dust emissions and reducing the need for water-based cleaning systems. The closed-loop design of the system ensures that any material that may escape is captured and returned to the process, preventing waste and environmental pollution. This aligns with the growing emphasis on sustainable practices in the chemical and manufacturing industries.
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial application has unique requirements. The company offers customized pneumatic conveying solutions that can be scaled to meet the specific needs of a facility. Whether it's a small-scale operation or a large industrial plant, the system can be adjusted to handle varying volumes of sodium carbonate. The modular design of the equipment allows for easy expansion or modification as the business grows. This flexibility ensures that the investment in the conveying system remains relevant and effective over time.
Conclusion
As the demand for efficient and reliable sodium carbonate transport continues to grow, advanced pneumatic conveying systems like those from Shandong HeadPowder Engineering Co., Ltd. are becoming increasingly important. By combining modern technology with practical design, HeadPowder's solutions offer significant advantages over traditional mechanical methods. The company's commitment to quality, efficiency, and sustainability makes their pneumatic conveying systems an excellent choice for industries looking to optimize their material handling processes. Whether it's for glass production, chemical manufacturing, or water treatment, HeadPowder's approach provides a robust and effective solution for sodium carbonate conveying.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc
Điện thoại
WeChatTư vấn
Lên đầu