Chuyên sâu trong lĩnh vực vật liệu rời công nghiệp, cung cấp giải pháp môi trường thông minh tích hợp cho phối trộn tự động, cấp liệu tập trung, khử lưu huỳnh và khử nitơ khô!
Urea granules are a critical component in modern agricultural and industrial applications, requiring efficient and reliable conveying systems to ensure smooth material handling. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for urea granule conveying, catering to diverse operational needs across various industries. This article explores the primary methods used for urea granule conveyance, highlighting the key features and applications of each approach.
Pneumatic Conveying Systems for Urea Granules

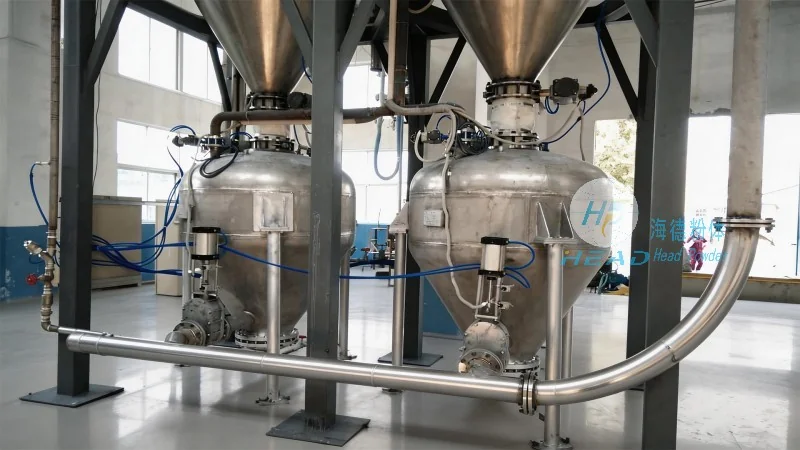
Pneumatic conveying, also known as air-based transport, is a popular method for urea granule handling due to its ability to transport materials over long distances and in enclosed systems. This technique involves using compressed air to move granules through a pipeline. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use positive pressure to push material forward, while vacuum systems use negative pressure to pull material. For urea granules, pressure systems are often preferred as they can handle higher material loads and are more suitable for long-distance transport. The key components of a pneumatic conveying system include a blower, a hopper for material storage, a conveyor line, and a discharge point. The system must be designed to prevent material buildup and ensure consistent air flow to maintain efficiency. Shandong HeadPowder Engineering Co., Ltd. offers customized pneumatic conveying solutions that incorporate advanced control systems to optimize performance and reduce energy consumption. These systems are particularly effective for applications where dust control and material containment are critical, such as in agricultural fertilizer plants or industrial processing facilities.
Mechanical Conveying Methods: Screw and Belt Conveyors
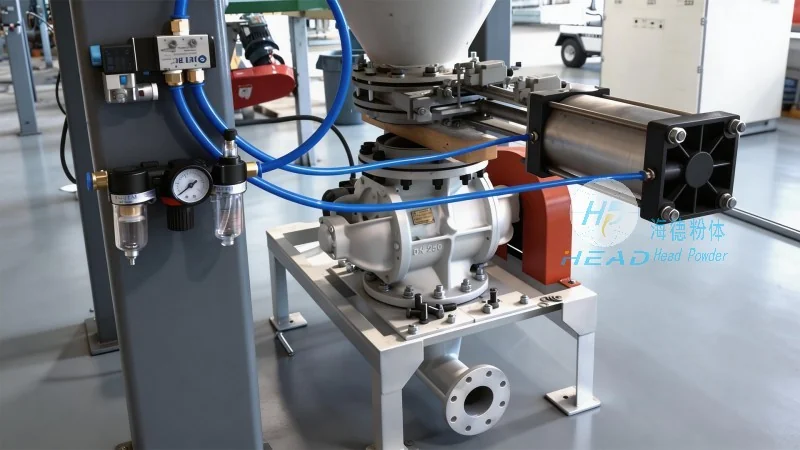
Mechanical conveying systems rely on mechanical components to move urea granules, offering a cost-effective alternative to pneumatic methods for shorter distances or lower material volumes. The most common types include screw conveyors and belt conveyors. Screw conveyors use a rotating screw (auger) to push material forward through a trough. They are ideal for horizontal or slight incline transport and are suitable for handling granular materials like urea. The design of the screw conveyor, including the pitch and diameter of the screw, is critical to ensure efficient material movement without excessive wear. Belt conveyors, on the other hand, use a continuous belt to transport granules, often in combination with idlers and pulleys to maintain tension and direction. These systems are well-suited for longer horizontal distances and can handle larger volumes of material. Both screw and belt conveyors are designed to minimize material spillage and provide reliable operation under various conditions. Shandong HeadPowder Engineering Co., Ltd. manufactures high-quality mechanical conveying equipment that meets industry standards for durability and performance. Their products are engineered to withstand the abrasive nature of urea granules and are available in various configurations to suit specific operational requirements.
Bucket Elevators and Their Role in Urea Granule Transport
Bucket elevators are vertical or inclined mechanical systems that use buckets attached to a chain or belt to lift and transport urea granules. This method is particularly effective for vertical or steep incline transport, allowing for efficient movement of material from lower to higher levels. The buckets are filled at the bottom of the elevator and discharged at the top, making it suitable for applications where elevation changes are required. Bucket elevators are known for their high capacity and ability to handle large volumes of material in a compact footprint. They are commonly used in fertilizer plants to move urea granules from storage silos to processing units or to different levels of the facility. Shandong HeadPowder Engineering Co., Ltd. provides robust bucket elevator solutions that incorporate wear-resistant materials to extend the service life of the equipment. These systems are designed to operate reliably under heavy loads and are equipped with safety features to prevent material spillage and ensure operator safety.
Factors to Consider When Choosing a Conveying Method
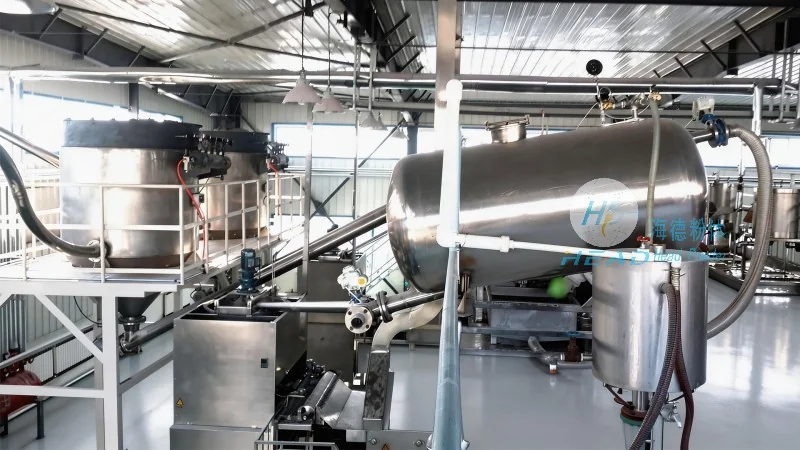
The selection of an appropriate urea granule conveying method involves evaluating several key factors to ensure optimal performance and cost-effectiveness. First, the distance and layout of the material transport route are critical. For short distances, mechanical conveyors like screw or belt systems may be sufficient, while pneumatic or bucket elevators are better suited for longer or vertical transport. Second, the volume of material to be conveyed plays a significant role. High-volume applications often require pneumatic or bucket elevators to maintain throughput, whereas low-volume needs can be handled by smaller mechanical systems. Third, environmental considerations, such as the need for dust control or material containment, influence the choice of system. Pneumatic conveying systems excel in enclosed environments, while mechanical systems may require additional dust suppression measures. Fourth, the budget and operational costs are important considerations. Mechanical systems generally have lower initial costs and lower energy consumption compared to pneumatic systems, which may have higher energy requirements but offer greater flexibility in terms of distance and layout. Shandong HeadPowder Engineering Co., Ltd. assists clients in evaluating these factors and selecting the most suitable conveying method for their specific needs, ensuring that the chosen system aligns with their operational goals and budget constraints.
Conclusion: Tailored Solutions for Urea Granule Conveying
Efficient urea granule conveying is essential for maintaining productivity and ensuring the safe handling of this critical material. Shandong HeadPowder Engineering Co., Ltd. offers a range of advanced conveying solutions, including pneumatic, mechanical, and bucket elevator systems, designed to meet the diverse needs of agricultural and industrial applications. By understanding the specific requirements of each operation, the company provides customized equipment that enhances performance, reduces maintenance costs, and ensures compliance with industry standards. Whether for short horizontal transport or long vertical distances, their solutions are engineered to deliver reliable and efficient material handling. With a focus on quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. remains a trusted partner for businesses seeking to optimize their urea granule conveying processes.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc
Điện thoại
WeChatTư vấn
Lên đầu