Chuyên sâu trong lĩnh vực vật liệu rời công nghiệp, cung cấp giải pháp môi trường thông minh tích hợp cho phối trộn tự động, cấp liệu tập trung, khử lưu huỳnh và khử nitơ khô!
When it comes to managing the flow of cocoa powder in industrial settings, selecting the appropriate pneumatic conveying system is crucial for maintaining efficiency, product quality, and operational safety. The choice of system directly impacts how smoothly cocoa powder is transported from storage to processing equipment, and even to packaging lines. With various options available, understanding the specific requirements of your cocoa powder handling process is key to making an informed decision. This guide aims to provide insights into the factors that influence the selection of a suitable pneumatic conveying system, with a focus on the expertise and solutions offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
Understanding the Importance of Pneumatic Conveying for Cocoa Powder


Cocoa powder, with its fine particle size and hygroscopic nature, presents unique challenges in material handling. Traditional methods like belt conveyors or bucket elevators may not be ideal due to the risk of dust generation, product degradation, or contamination. Pneumatic conveying systems offer a more controlled and hygienic solution by using air to transport the powder through a sealed system. This not only minimizes dust exposure but also helps maintain the quality and freshness of the cocoa powder. For industries that prioritize product integrity and operational efficiency, pneumatic conveying has become a preferred method for cocoa powder transport.
Key Considerations in Choosing a Pneumatic Conveying System
Before selecting a pneumatic conveying system for cocoa powder, several factors must be carefully evaluated. The first consideration is the type of system: positive pressure, negative pressure, or a combination of both. Positive pressure systems use compressed air to push the material through the pipeline, while negative pressure systems use vacuum to draw the material in. The choice depends on the distance, elevation changes, and the nature of the material. For cocoa powder, which is typically light and fine, both systems can be effective, but the system's design must ensure minimal pressure drop and consistent flow. Another critical factor is the material's properties, such as particle size, density, and flowability. Cocoa powder's fine particles can lead to caking or bridging in the hopper, which may affect the system's performance. Therefore, the design of the hopper and feeder must be optimized to prevent these issues and ensure smooth material discharge. Additionally, the system's capacity and the required conveying distance are important. The layout of the facility, including the location of storage silos, processing equipment, and packaging stations, will influence the pipeline design and the overall system configuration. It's also essential to consider the system's maintenance requirements and the availability of spare parts. A well-designed system should be easy to clean and maintain, with components that are resistant to corrosion and wear from the cocoa powder.
HeadPowder's Expertise in Cocoa Powder Pneumatic Conveying Solutions

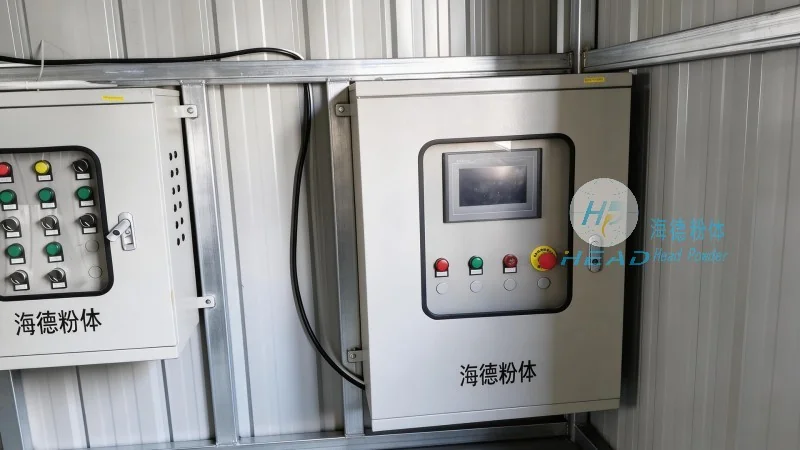
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of cocoa powder handling. With years of experience in the industry, HeadPowder has developed a deep understanding of the challenges associated with cocoa powder transport and has engineered solutions that address these issues effectively. The company's team of engineers works closely with clients to assess their operational requirements, material characteristics, and facility layout to design a system that maximizes efficiency and minimizes downtime. HeadPowder offers a range of pneumatic conveying systems, including positive pressure, negative pressure, and hybrid systems, each designed to handle the unique properties of cocoa powder. The systems are constructed using high-quality materials, such as stainless steel, to ensure durability and resistance to corrosion from the cocoa powder and any moisture present. The company also provides comprehensive support, including installation, commissioning, and after-sales maintenance, to ensure that the system operates at its best. By choosing HeadPowder's solutions, clients can benefit from a reliable and efficient system that meets their specific cocoa powder handling needs.
Conclusion: Making the Right Choice for Your Cocoa Powder Handling Process
Selecting the right pneumatic conveying system for your cocoa powder handling process is a critical decision that can significantly impact your operational efficiency and product quality. By considering factors such as system type, material properties, capacity, and maintenance requirements, you can choose a system that best suits your needs. Shandong HeadPowder Engineering Co., Ltd. offers expert solutions tailored to the unique challenges of cocoa powder transport, ensuring that your system is designed for optimal performance and longevity. With their experience and commitment to quality, HeadPowder is a trusted partner for businesses looking to enhance their cocoa powder handling operations. Whether you are a new or existing facility, HeadPowder's customized pneumatic conveying systems can help you achieve efficient, safe, and reliable cocoa powder transport, supporting your production goals and maintaining the high standards of your products.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc
Điện thoại
WeChatTư vấn
Lên đầu