Chuyên sâu trong lĩnh vực vật liệu rời công nghiệp, cung cấp giải pháp môi trường thông minh tích hợp cho phối trộn tự động, cấp liệu tập trung, khử lưu huỳnh và khử nitơ khô!
When it comes to handling camellia seeds in industrial processing, selecting an appropriate pneumatic conveying system is crucial for maintaining efficiency, product quality, and operational safety. The choice of system directly impacts how effectively seeds are transported from one stage of processing to another, such as from storage silos to processing equipment or between different processing units. A well-designed system can minimize product degradation, reduce labor costs, and enhance overall production throughput.
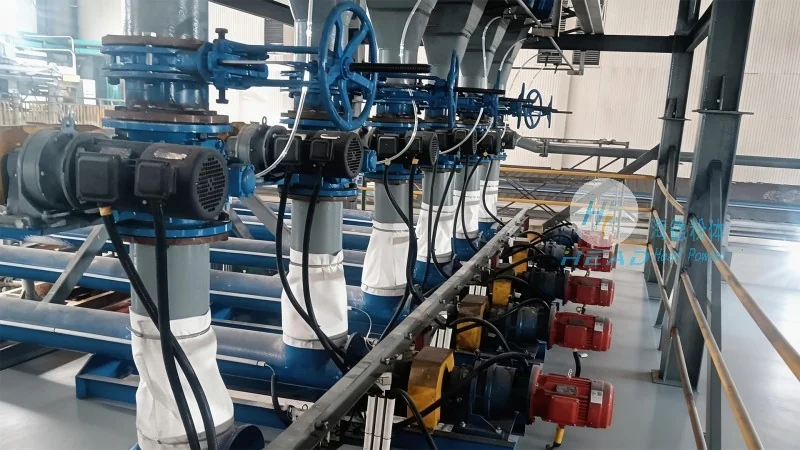
Key Considerations for Selecting a Pneumatic Conveying System
Several factors must be considered when choosing a pneumatic conveying system for camellia seed applications. These include the seed's physical properties—such as particle size, density, moisture content, and flowability—along with the required conveying distance and volume. The system's pressure type (positive pressure, negative pressure, or a combination) is also critical. Positive pressure systems use air to push material through pipelines, while negative pressure systems use suction to draw material. The choice depends on the specific handling requirements and the layout of the processing facility.
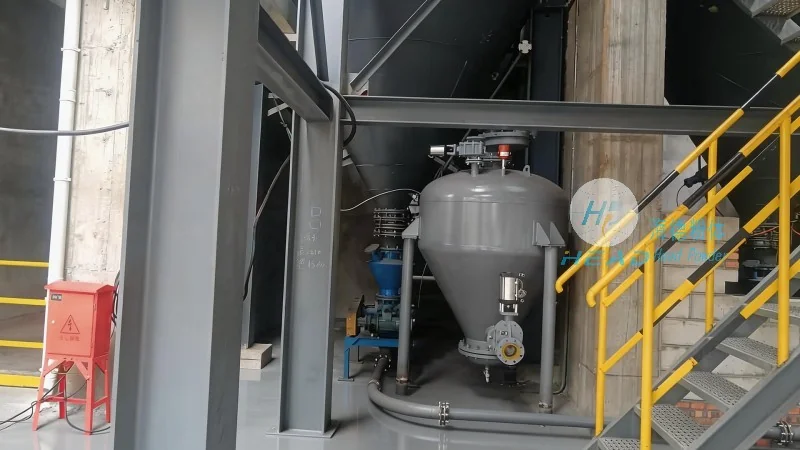
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying systems, specializes in designing and manufacturing customized solutions tailored to the unique needs of camellia seed processing facilities. With years of experience in the industry, HeadPowder understands the challenges associated with handling delicate seeds and has developed advanced systems that ensure minimal product breakage and consistent performance. The company's engineers work closely with clients to assess their specific requirements, including processing capacity, space constraints, and budget considerations, to deliver optimal solutions.
Customized Pneumatic Conveying Systems for Camellia Seeds
HeadPowder offers a range of pneumatic conveying systems suitable for camellia seed handling, including dilute phase and dense phase systems. Dilute phase systems are ideal for short to medium conveying distances and moderate flow rates, while dense phase systems are better suited for longer distances or when handling more abrasive or delicate materials. The company's systems are equipped with high-quality components, such as efficient air blowers, durable pipelines, and advanced control systems, ensuring reliable operation and long service life. Additionally, HeadPowder provides comprehensive support, including installation, commissioning, and maintenance services, to ensure clients achieve maximum return on their investment.
Benefits of Choosing HeadPowder's Pneumatic Conveying Systems

Implementing a HeadPowder pneumatic conveying system for camellia seed handling offers numerous benefits. These include improved product quality by reducing handling-related damage, increased operational efficiency through automated material transport, and enhanced safety by minimizing manual handling of seeds. The systems are also designed to be energy-efficient, helping clients reduce operational costs while maintaining high performance standards. Furthermore, HeadPowder's commitment to quality and customer satisfaction ensures that clients receive systems that meet their specific needs and comply with industry standards.
Contact Information for HeadPowder Engineering
For more information about HeadPowder's pneumatic conveying systems for camellia seed handling, please contact our team at Shandong HeadPowder Engineering Co., Ltd. Located in Shandong, China, our company is dedicated to providing innovative and reliable solutions that enhance the efficiency and profitability of your processing operations. We welcome the opportunity to discuss your specific requirements and help you select the right system for your camellia seed handling process.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc
Điện thoại
WeChatTư vấn
Lên đầu