Chuyên sâu trong lĩnh vực vật liệu rời công nghiệp, cung cấp giải pháp môi trường thông minh tích hợp cho phối trộn tự động, cấp liệu tập trung, khử lưu huỳnh và khử nitơ khô!
Efficient and environmentally friendly material handling solutions are increasingly critical in modern industrial operations. Among these, the pneumatic conveying of sodium bicarbonate stands out as a versatile and sustainable approach to transporting this widely used chemical. This article explores the benefits, applications, and technical aspects of sodium bicarbonate pneumatic conveying, highlighting how it addresses the challenges of traditional material transport methods while aligning with contemporary industrial standards.
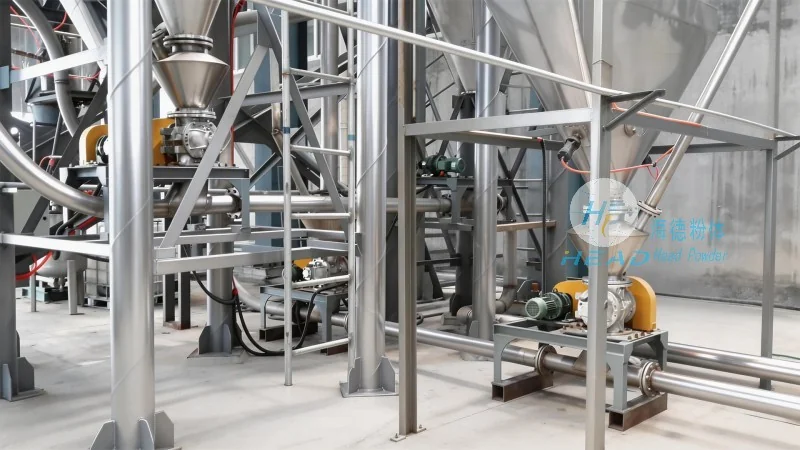
Understanding Sodium Bicarbonate Pneumatic Conveying
Sodium bicarbonate, commonly known as baking soda, is a versatile chemical used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. Conventional material handling methods for sodium bicarbonate often involve bulk handling equipment like conveyors or trucks, which can be inefficient, costly, and environmentally unfriendly due to dust generation and energy consumption. Pneumatic conveying offers a superior alternative by using air to transport the material, reducing the need for mechanical components and minimizing environmental impact.
The Advantages of Pneumatic Conveying for Sodium Bicarbonate

One of the primary advantages of pneumatic conveying is its efficiency in transporting sodium bicarbonate. Unlike traditional methods, pneumatic systems can handle fine powders and granules with minimal loss, ensuring consistent product quality. The process is also highly scalable, allowing for both small-scale and large-scale operations. Additionally, pneumatic conveying reduces labor costs by automating the material transport process and minimizing the need for manual handling, which is particularly beneficial for hazardous materials like sodium bicarbonate.
Environmental Benefits and Sustainability
Environmental sustainability is a key consideration in modern industrial practices, and pneumatic conveying of sodium bicarbonate offers significant advantages in this regard. Traditional bulk handling methods often generate dust and emissions, contributing to air pollution and health hazards. Pneumatic systems, on the other hand, are enclosed and use filtered air, reducing dust emissions and improving workplace safety. Furthermore, the energy efficiency of pneumatic conveying systems is higher compared to mechanical conveyors, as they utilize compressed air to move material with less energy consumption. This makes pneumatic conveying an environmentally friendly choice that aligns with global sustainability goals.
Technical Considerations in Pneumatic Conveying Systems
The success of sodium bicarbonate pneumatic conveying depends on several technical factors. The design of the conveying system must consider the properties of sodium bicarbonate, such as its particle size, density, and flow characteristics. Proper system design ensures smooth and continuous material transport, preventing blockages and ensuring consistent performance. Key components of a pneumatic conveying system include the air compressor, conveying lines, and material feeders. The choice of materials for these components is critical, as they must withstand the corrosive nature of sodium bicarbonate and the effects of air pressure. Additionally, the system must be equipped with appropriate filtration and dust collection equipment to maintain air quality and comply with environmental regulations.

Applications in Industrial Settings
Sodium bicarbonate pneumatic conveying is widely used in various industrial applications. In the food industry, it is used for transporting baking soda used in baking and food processing, ensuring hygiene and efficiency. In pharmaceutical manufacturing, pneumatic conveying is employed to transport sodium bicarbonate used in drug formulations, maintaining product purity and reducing contamination risks. The chemical industry also utilizes pneumatic conveying for transporting sodium bicarbonate used in chemical reactions and processes, where consistent material flow is essential for product quality. Additionally, in the agricultural sector, pneumatic conveying can be used to transport sodium bicarbonate as a fertilizer or soil amendment, improving agricultural productivity.
HeadPowder: A Leader in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pneumatic conveying solutions for sodium bicarbonate and other materials. With years of experience in the industry, HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems that meet the specific needs of its clients. The company's expertise lies in understanding the unique properties of sodium bicarbonate and developing systems that optimize material transport while minimizing environmental impact. HeadPowder's team of engineers and technicians work closely with clients to assess their operational requirements and provide tailored solutions that enhance efficiency and sustainability.
Customized Solutions for Diverse Needs

HeadPowder recognizes that each industrial application has unique requirements, and therefore, offers customized pneumatic conveying solutions. The company's approach involves a thorough analysis of the client's material handling needs, including the type and quantity of sodium bicarbonate, the distance of transport, and the environmental and safety standards. Based on this analysis, HeadPowder designs and manufactures systems that are optimized for performance, reliability, and cost-effectiveness. The company's customized solutions may include different types of pneumatic conveying systems, such as pressure or vacuum systems, depending on the specific requirements. Additionally, HeadPowder provides comprehensive support services, including installation, maintenance, and technical support, ensuring that clients can maximize the benefits of their pneumatic conveying systems.
Ensuring Quality and Reliability
Quality and reliability are paramount in the design and operation of pneumatic conveying systems. HeadPowder adheres to strict quality control standards to ensure that its systems meet the highest industry standards. The company uses high-quality materials and components in its systems, ensuring durability and long-term performance. Regular maintenance and inspection of the systems are also essential to maintain optimal performance and prevent breakdowns. HeadPowder's technical support team provides ongoing assistance to clients, addressing any issues that may arise and ensuring that the systems operate efficiently. This commitment to quality and reliability has made HeadPowder a trusted partner for many industrial clients.
Conclusion
Sodium bicarbonate pneumatic conveying is a highly efficient and environmentally friendly solution for material handling in various industries. By using air to transport the material, this method reduces the need for mechanical components, minimizes dust emissions, and improves workplace safety. The technical advancements in pneumatic conveying systems have made them more reliable and efficient, making them an attractive option for industrial operations. HeadPowder, with its expertise and customized solutions, plays a crucial role in providing effective pneumatic conveying systems for sodium bicarbonate and other materials. As industrial operations continue to prioritize efficiency and sustainability, pneumatic conveying of sodium bicarbonate will remain a key solution for material handling in the future.
 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc
Điện thoại
WeChatTư vấn
Lên đầu